Mold making in China is the single largest upfront cost in injection molding — and the step where most sourcing mistakes happen. We have seen a $5,000 mold from a careful supplier produce 100,000 consistent parts, while a $3,000 mold from another shop drifted out of tolerance at 10,000 shots. The difference is almost never the machine — it is the steel selection, the DFM review, and the quality verification before production begins.
What is mold making in China?
Mold making in China is the design, machining, and trial-testing of injection molds (tooling) by Chinese mold shops for product teams worldwide. A mold is the steel tool that forms plastic parts: molten resin is injected into its cavity, cools, and is ejected as a finished part. Chinese mold making covers three tiers 鈥?prototype or soft molds (1-2 cavities, 5,000-50,000 shots), pre-hardened steel molds such as P20 and 718H (1-16 cavities, 100,000-500,000 shots), and hardened steel molds such as H13, S136 and NAK80 (1-64 cavities, 500,000-1,000,000+ shots). The tier you need is determined by your production volume and material, not by price alone.
1. Mold Types and When to Use Each
| Mold Type | Cavities | Life (shots) | Best For |
|---|---|---|---|
| Prototype / soft mold | 1-2 | 5,000–50,000 | Design validation, bridge production |
| Pre-hardened steel (P20, 718H) | 1-16 | 100,000–500,000 | Mid-volume consumer products |
| Hardened steel (H13, S136, NAK80) | 1-64 | 500,000–1,000,000+ | High-volume, abrasive materials |
| Hot runner mold | 2-32 | Varies | Reduced waste, faster cycles |
We recommend P20 for general-purpose production, H13 when heat resistance matters for engineering resins, and S136 for corrosion resistance in medical and optical applications. Choosing the wrong steel grade adds cost and shortens tool life — we flag this in every DFM report.
2. What Drives Mold Making Cost in China
When sourcing mold making in China, understanding these cost drivers helps you compare quotes accurately.
| Cost Driver | Impact | Why |
|---|---|---|
| Cavity count | High | Each cavity adds machining, EDM, polishing time |
| Steel grade | Medium | H13 costs 1.5–2× P20 in material and machining |
| Part complexity | High | Undercuts, threads, side actions require slides/lifters |
| Surface finish | Medium | SPI A1 mirror takes significantly more polishing time |
| Tolerance requirements | High | ±0.02mm requires precision grinding and process control |
| Hot runner system | High | Adds $2,000–8,000 but cuts cycle time and material waste |
We have seen quotes for the same part vary 2–3× between suppliers — the difference is nearly always in the details above. Our quotes break down each cost driver so you can compare apples to apples.
Mold making in China: key numbers at a glance
These are the figures that determine mold cost and tool life. Each one is verifiable from a supplier’s quote and steel certificates.
- Prototype / soft mold life: 5,000-50,000 shots, 1-2 cavities
- P20 / 718H pre-hardened steel life: 100,000-500,000 shots, 1-16 cavities
- H13 / S136 / NAK80 hardened steel life: 500,000-1,000,000+ shots, 1-64 cavities
- H13 steel cost premium over P20: 1.5-2x in material and machining
- Hot runner system premium: adds roughly $2,000-8,000 to tooling cost, but cuts cycle time and material waste
- Tolerance threshold that changes cost: holding 卤0.02 mm requires precision grinding and process control, not standard machining
- Quote spread across suppliers: the same part has been quoted at 2-3x differences between shops, driven almost entirely by cavity count, steel grade, part complexity, surface finish, tolerance, and hot runner choice
The practical takeaway: two quotes for the same part are rarely comparable unless each one itemizes cavity count, steel grade, tolerance band, surface finish (SPI grade), and whether a hot runner is included.
3. DFM Checklist — Before You Cut Steel
Our DFM review for every mold making project checks these seven points before steel is ordered:
- Gate location: Does it allow balanced filling of all cavities?
- Venting: Are vents deep enough to let gas escape without creating flash?
- Ejection: Are ejector pins positioned on non-cosmetic surfaces?
- Draft angles: Minimum 0.5° on core, 1° on cavity for textured surfaces
- Wall thickness: Uniform? Sudden changes cause sink marks
- Cooling channels: Positioned for uniform cooling and shortest cycle time?
- Steel-to-resin compatibility: Is the steel grade suitable for your material? Glass-filled nylon demands hardened steel.
A competent mold maker sends a DFM report with the quote. If you receive a price without design feedback, they have not looked at your part. We include this as standard.
4. Quality Verification Before Acceptance
Before you accept a mold from any supplier, verify these five items:
- First-article inspection: Dimensional report on the first shots off the mold — minimum acceptable standard.
- Process capability (Cpk): For production molds, Cpk above 1.33 on critical-to-quality dimensions proves the process can hold tolerance.
- Mold trial report: Cycle time, injection pressure, clamp force, and processing notes — if they are not documented, future runs cannot be replicated.
- Steel certification: Material certificates confirming the steel grade you paid for.
- Warranty terms: Minimum shot count or time period, with clarity on maintenance coverage.
5. Common Sourcing Pitfalls
| Pitfall | Consequence | Prevention |
|---|---|---|
| Price-only selection | Soft steel degrades after 20K shots | Require steel grade in your quote |
| Skipping DFM | Tooling issues found after steel is cut — rework costs more than the original mold | Require DFM report before cutting begins |
| No trial report | Future production runs cannot be replicated | Documented processing parameters |
| Unclear mold ownership | Dispute if switching suppliers | Mold ownership clause in your PO |
| Missing spare parts | Broken ejector pin halts production for two weeks | Order spare ejector pins, springs, and heaters with the mold |
6. How to Evaluate a Mold Maker for Your Project
The quality of mold making in China varies widely between suppliers. Here is how we evaluate a shop before committing to a build.
Before you commit to a mold build, we recommend checking four things:
- Equipment: Can their machines handle your mold size? A 500-ton press cannot run a mold built for a 1,200-ton machine.
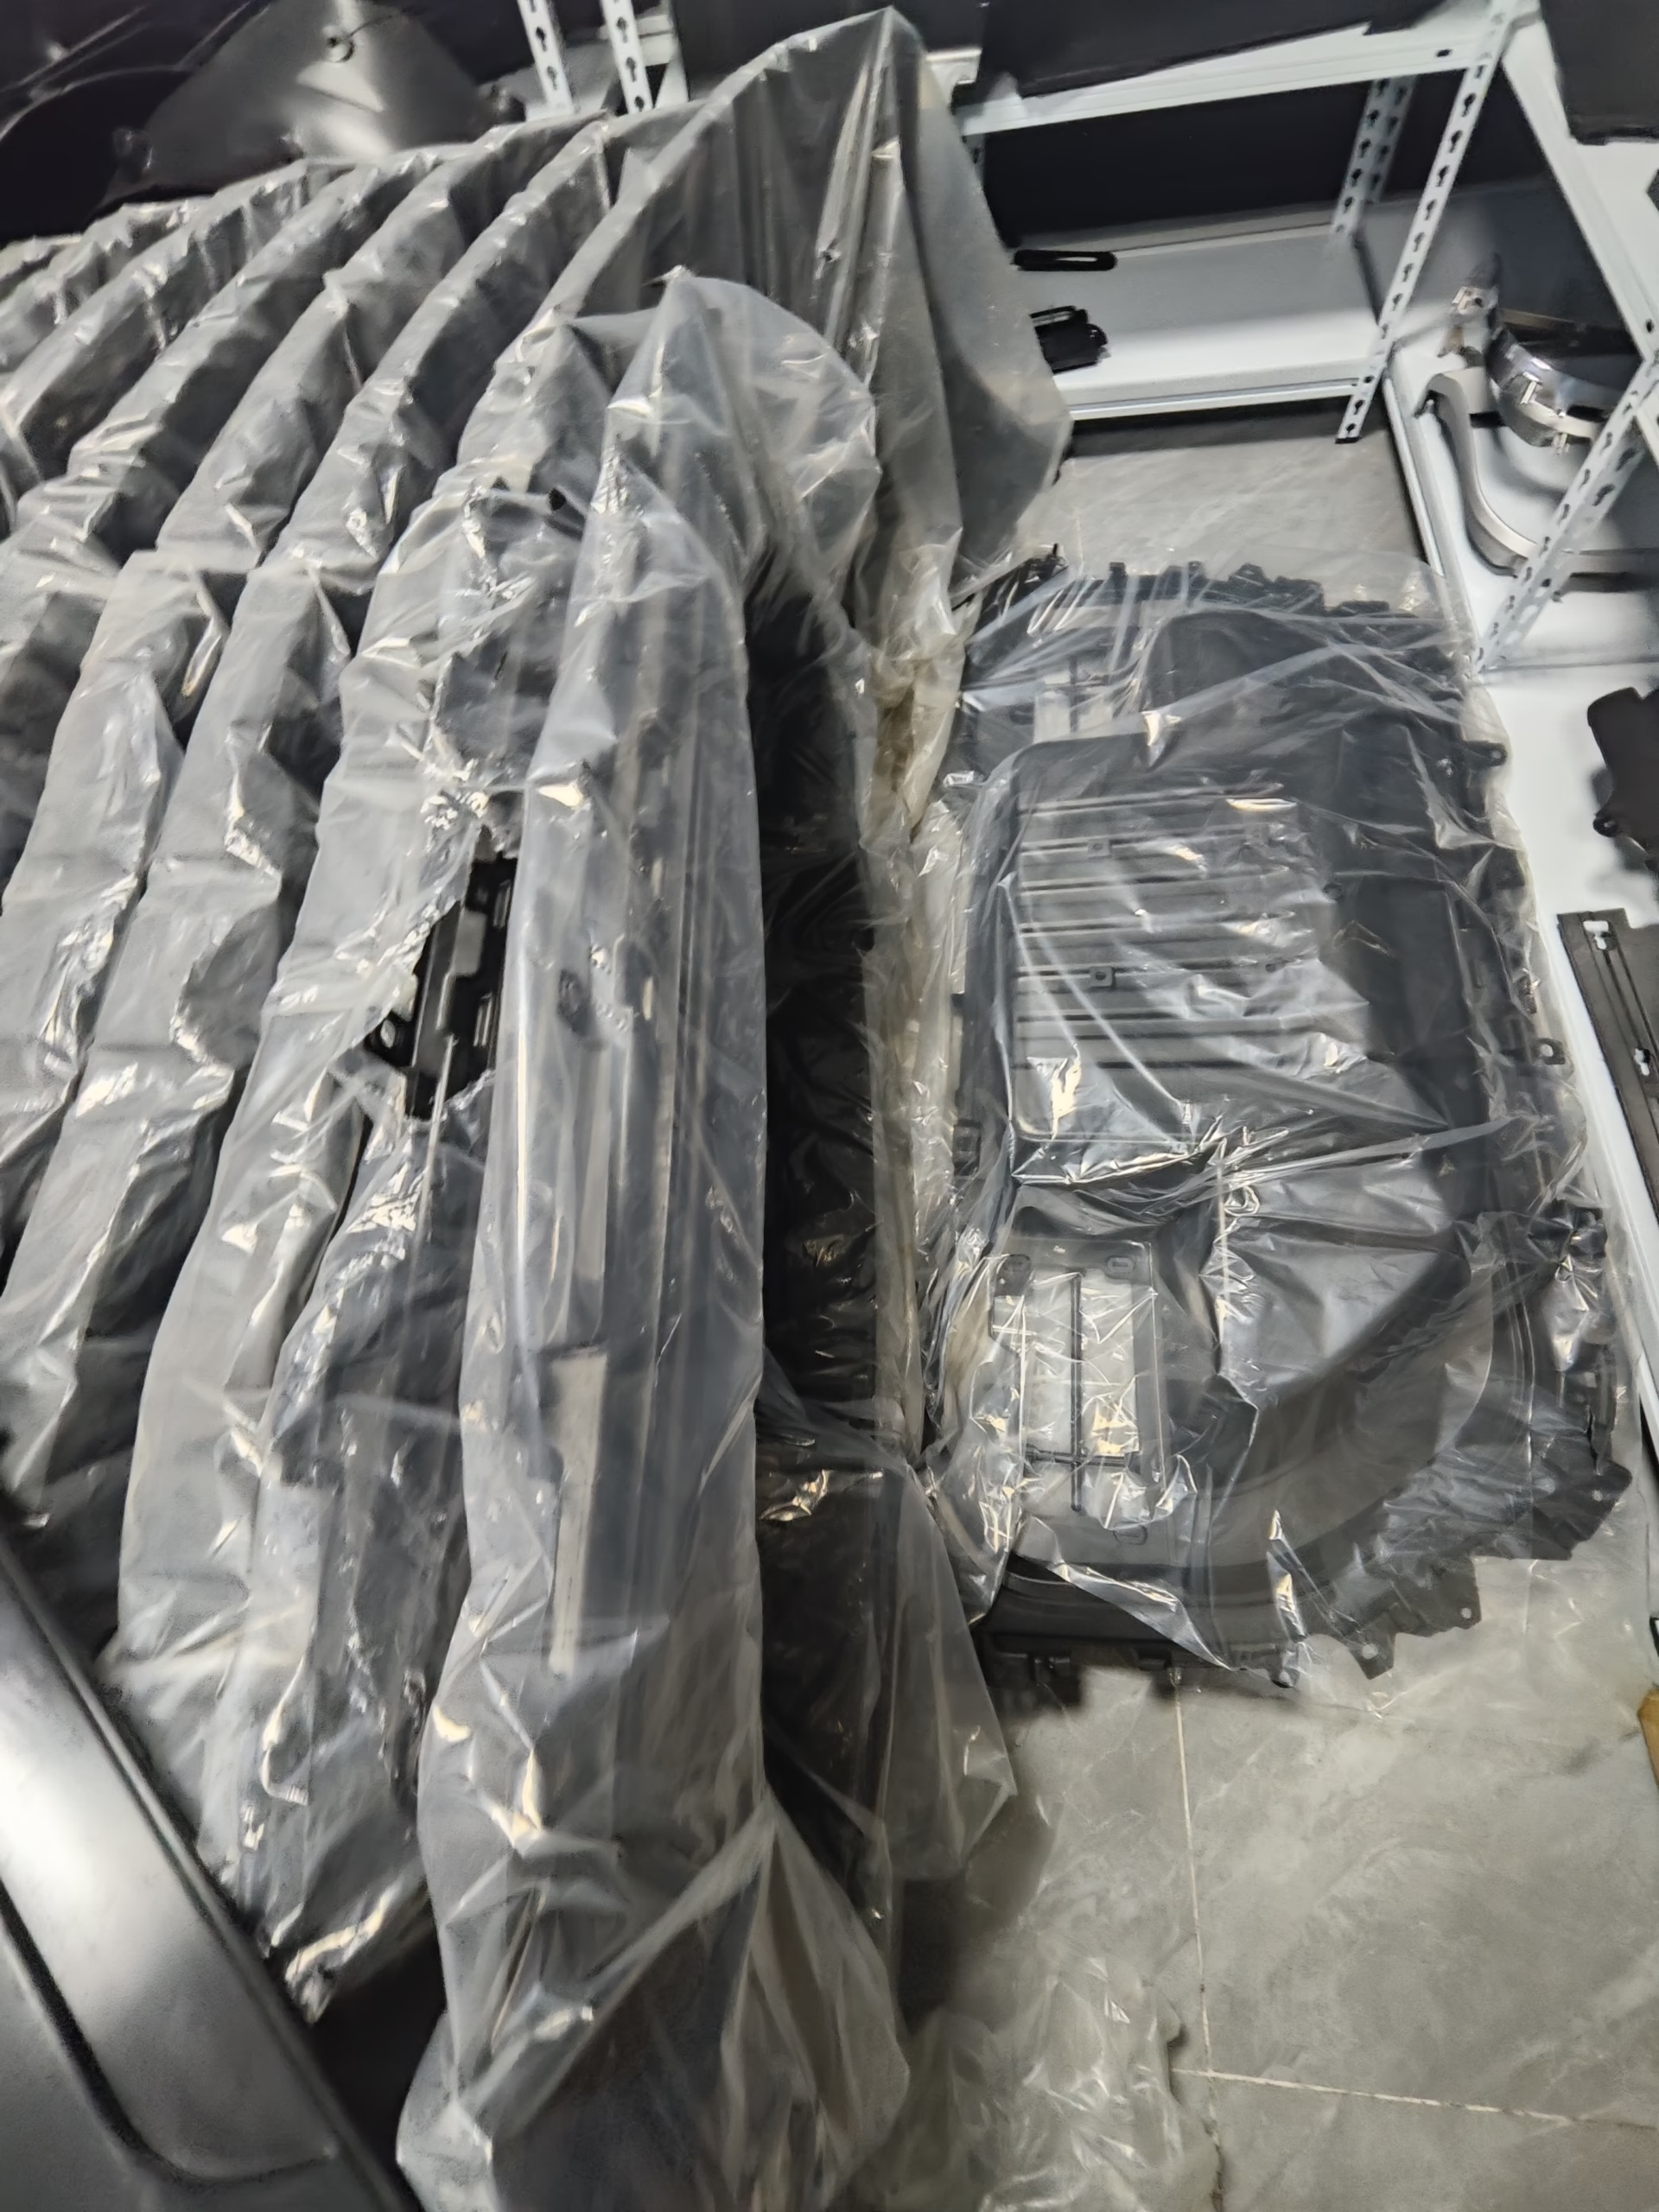
- Previous work: Ask for photos of molds similar to yours — not finished parts, but the actual molds. Mold photos reveal surface finish quality, cooling line layout, and general workmanship.
- DFM process: A mold maker who quotes without a DFM checklist is guessing.
- Communication: Do they respond in engineering terms, or only in price and delivery dates?
We have built molds ranging from single-cavity prototypes to 32-cavity high-volume production tools. Every project starts with a DFM review — no exceptions.
Mold making in China: frequently asked questions
How much does a mold cost in China?
Chinese mold pricing is driven by six factors: cavity count, steel grade, part complexity (undercuts, threads, side actions), surface finish (SPI grade), tolerance requirements, and whether a hot runner is used. A hot runner system alone adds roughly $2,000-8,000. Because these variables dominate price, the same part can be quoted at 2-3x differences between suppliers 鈥?a low quote usually reflects a softer steel or a skipped DFM review rather than genuine efficiency.
What is the difference between a prototype mold and a production mold?
A prototype (soft) mold uses lower-grade steel and runs 5,000-50,000 shots with 1-2 cavities 鈥?it exists to validate design and bridge to launch. A production mold uses pre-hardened (P20, 718H) or hardened steel (H13, S136, NAK80) and runs 100,000 to 1,000,000+ shots with up to 64 cavities. Choosing a prototype mold for production volume means replacing the tool mid-program; choosing a production mold too early locks in design decisions you may still change.
Which steel grade should I choose?
Use P20 for general-purpose mid-volume production. Choose H13 when heat resistance matters for engineering resins. Choose S136 when corrosion resistance is required, as in medical and optical applications. Glass-filled nylon and other abrasive materials demand hardened steel regardless of volume 鈥?softer steel wears out early. Every DFM report should state the recommended grade and the reason.
What is a DFM review, and why does it matter before cutting steel?
DFM (Design for Manufacturing) review is a structured engineering check of your part and mold design before steel is ordered. A competent mold maker’s DFM review covers at least seven points: gate location and balanced fill, venting depth, ejector pin placement on non-cosmetic surfaces, draft angles (minimum 0.5 degrees on core, 1 degree on textured cavity surfaces), uniform wall thickness, cooling channel layout, and steel-to-resin compatibility. A price without design feedback means the supplier has not examined your part. Rework after steel is cut costs more than the original mold.
How do I verify mold quality before accepting it?
Verify five items before acceptance: (1) first-article inspection with a dimensional report on the first shots; (2) process capability 鈥?Cpk above 1.33 on critical-to-quality dimensions for production molds; (3) a mold trial report documenting cycle time, injection pressure, clamp force and processing notes, without which future runs cannot be replicated; (4) steel certificates confirming the grade you paid for; (5) written warranty terms stating minimum shot count or time period and what maintenance covers.
Do I own the mold after it is built?
Only if your purchase order says so. Mold ownership must be stated explicitly as a clause in your PO. Without it, switching suppliers later can become a dispute over who holds the tool. Ask for the clause before the build starts, not after.
Can a Chinese supplier handle both prototyping and the mold?
Yes, and pairing them reduces risk. Building prototypes by CNC before committing to steel lets you validate fit, function and assembly on real parts, then cut the mold with validated geometry. The DFM review that precedes tooling works from the same CAD either way, so design changes found at prototype stage cost far less than changes found after steel is cut.
What spare parts should I order with the mold?
Order spare ejector pins, springs, and heaters together with the mold. A single broken ejector pin can halt production for two weeks waiting on a replacement, and matching non-standard components later is harder than buying them alongside the tool.